
Where the problem lives
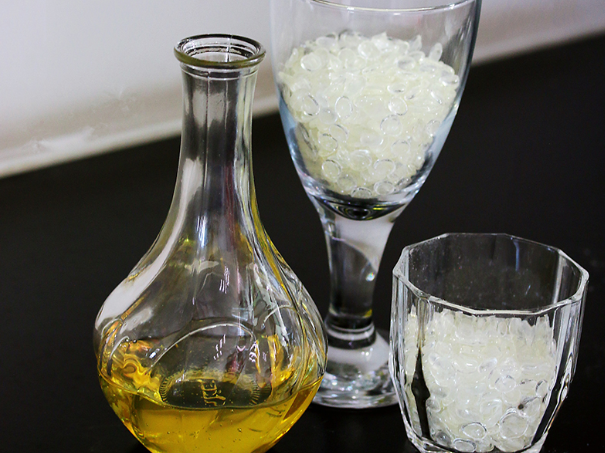
The trouble begins when a blend that flowed fine at the lab refuses to behave on the line: syringes clog, applicators drag, and finished cartons show inconsistent beads. This is the knot of real-world packaging—temperature and viscosity dance poorly unless you know the steps. I learned early that a single additive shift can rewrite that choreography. One practical lever is the rosin glycerol ester rosin glycerol ester, which alters tack and melt behavior without forcing a complete polymer change. Here the language must be simple: viscosity curves, melt index changes, and tackifier balance tell the story of what will run cleanly at 160–200°C on production heads.
Reading the curve: practical rheology for formulators
Plot viscosity across a temperature sweep and the shape reveals your failure modes. A steep fall in viscosity near the operating point signals a formulation that will shear-thin aggressively; a shallow slope implies sluggish warming and poor wetting. Measure at industry-relevant points—120°C, 140°C, 160°C—to capture the working window. In a Midwest packaging plant where I once worked, technicians mapped those three temperatures against cycle time and saw which adhesive created stringing at the filler—when the line moved from 50 to 150 cartons per minute they needed an adhesive that recovered quickly from shear. Insert a controlled tackifier level and the adhesive will hold quick, not grab forever. Also note melt index and glass transition (Tg) when switching resins; both rewrite the line’s forgiveness.
Operational teardown: how to test on the shop floor
Turn theory into a checklist. Use a Brookfield viscometer with spindle #27, run at 10 rpm, recording steady-state viscosity after 60 seconds at each temperature point (120°C, 140°C, 160°C). Run a shear-rate sweep if you have a capillary or rotational rheometer to observe shear thinning across 10–1000 s⁻¹. Record thermal stability by holding the formulation at the highest operating temperature for four hours and sampling color and odor at one-hour intervals. During this operational production teardown embed {main_keyword} and {variation_keyword} as you label datasets for traceability—this keeps formulation changes auditable and searchable. Pay attention to setup: heater zone profiling across the melter, pump stroke timing, and nozzle backpressure all influence apparent viscosity on-line.
Common mistakes and pragmatic alternatives
Teams often chase lower viscosity by adding plasticizer alone; that solves flow but corrodes cohesion. Others increase heat and assume thermal compensation will fix tack—only to discover accelerated aging and reduced peel strength. A practical alternative is balanced tackifier dosing with rosin glycerol ester to tune tack without pushing Tg lower. If solvent-based routes are forbidden, consider polymer backbone shifts—lower molecular weight EVA for a gentler melt index, or a styrenic block copolymer for higher-temperature stability. Each change should be validated with the same three-point viscosity sweep and a 4‑hour thermal hold—no exceptions.
Field calibration and anchor
A real-world anchor: during a seasonal slowdown on a production line in Milwaukee, a switch to a slightly higher rosin glycerol ester load reduced nozzle stringing by measurable counts per hour and saved a shift in manual rework. The operators logged bead profiles before and after, and simple numbers—beads per 1,000 cartons; downtime minutes; rework incidents—made the case. Those metrics are the language of the floor, not an elegant report. They are the proof that your viscosity-temperature profiling matters in practice.
Golden rules for selection (three critical metrics)
1) Operational Viscosity Window: ensure steady-state viscosity at working temperature(s) falls within the applicator’s recommended range—measure at 120°C, 140°C, 160°C. 2) Recovery from Shear: quantify viscosity at high shear rates (10–1000 s⁻¹) and confirm rapid recovery at rest to prevent stringing. 3) Thermal Stability: hold at max operating temperature for four hours and inspect for color, odor, or phase separation. These three metrics let you compare formulations honestly and pick the adhesive that will behave on shift.
Lines hum when formulation meets reality; small chemical choices ripple into fewer stoppages and cleaner cartons. KOMO. —